Get Your Free Quote…!
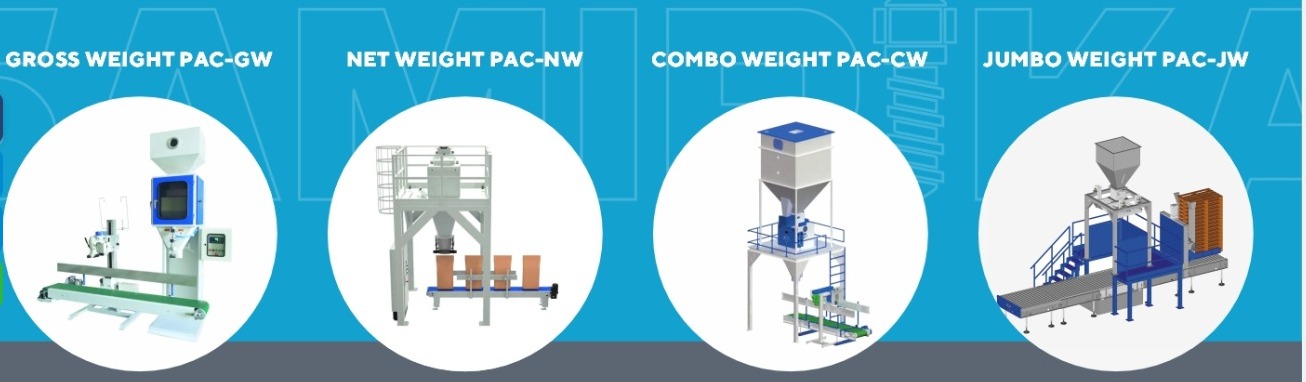
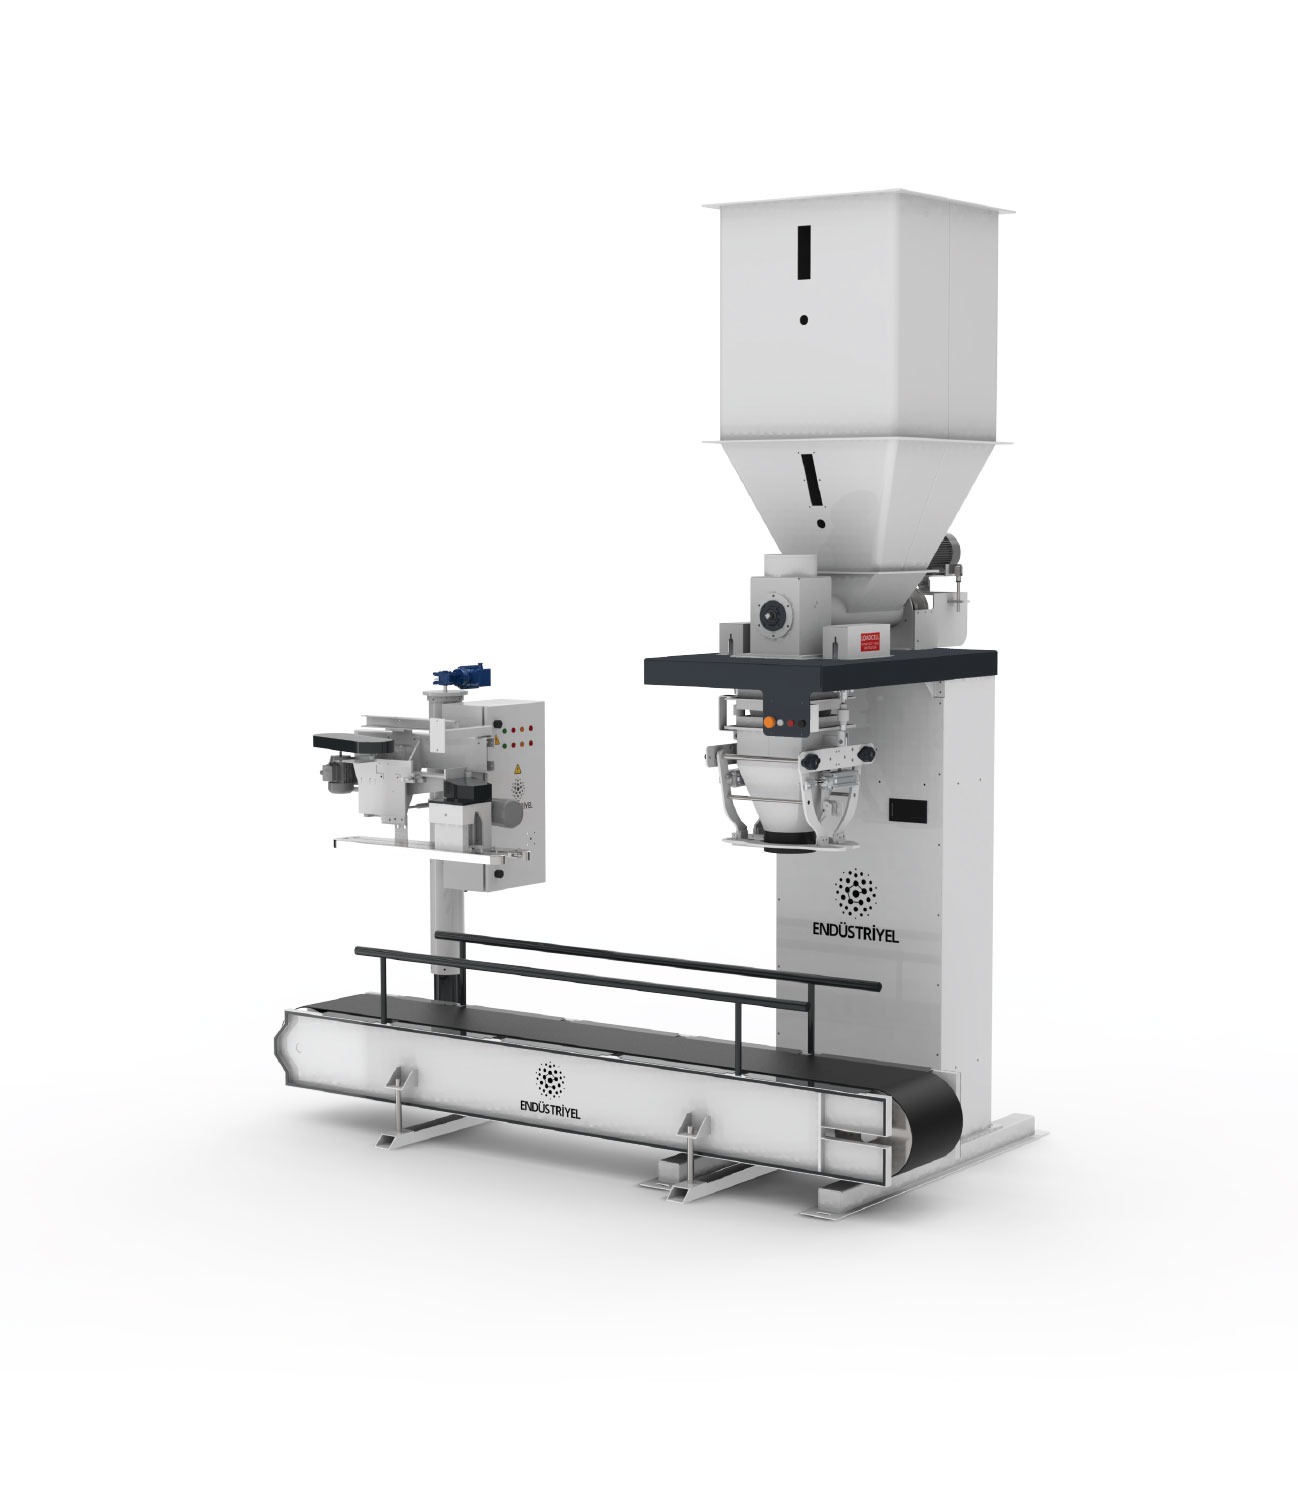
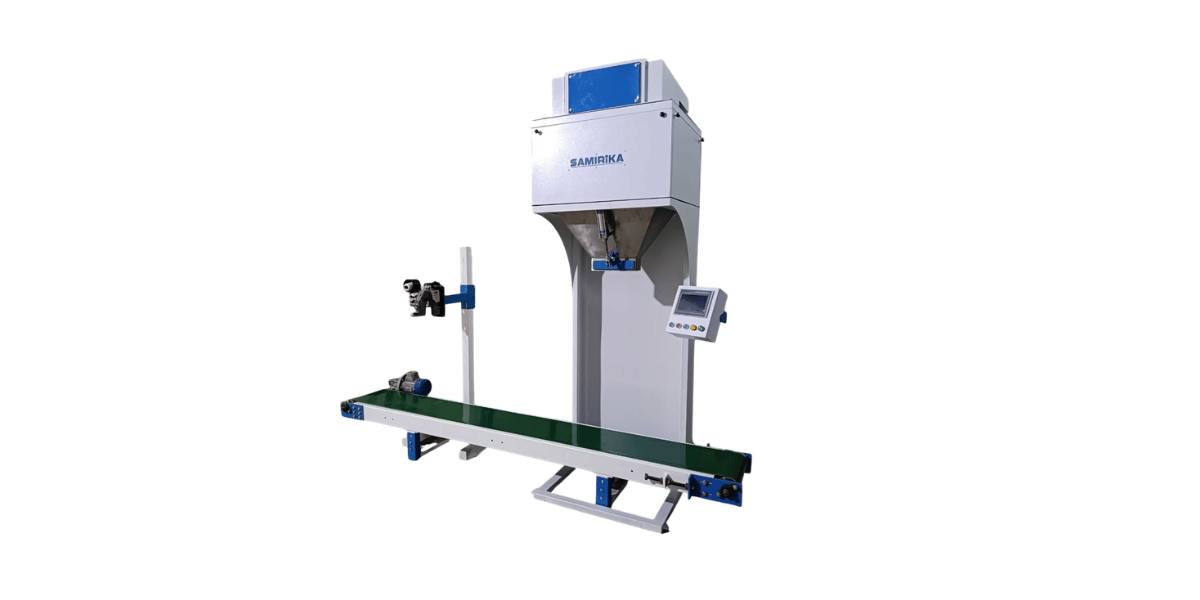
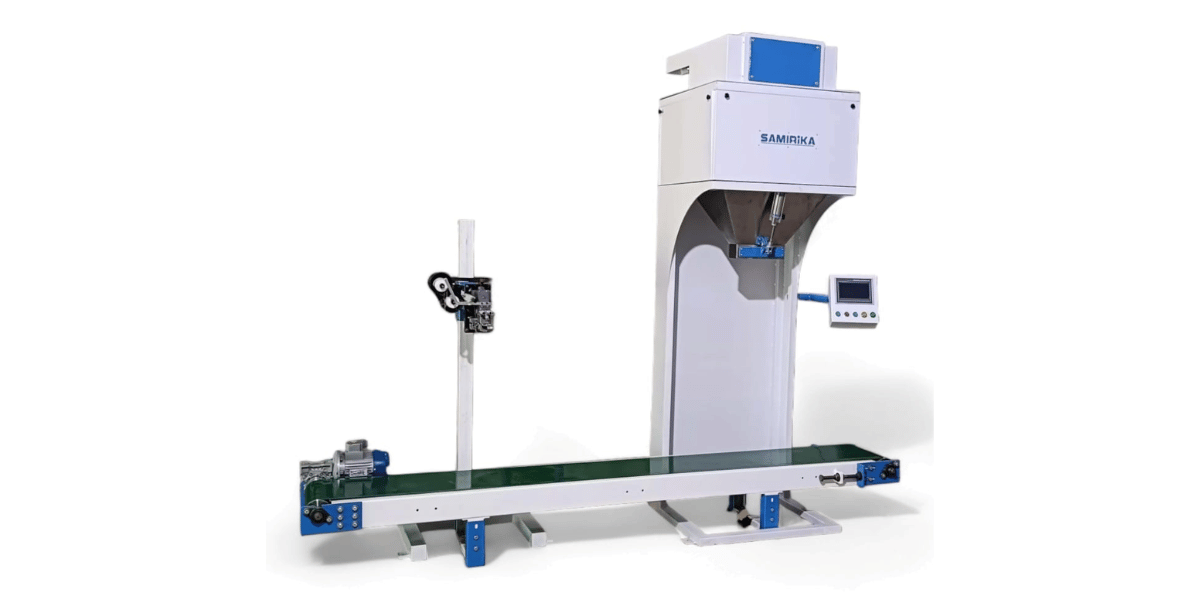
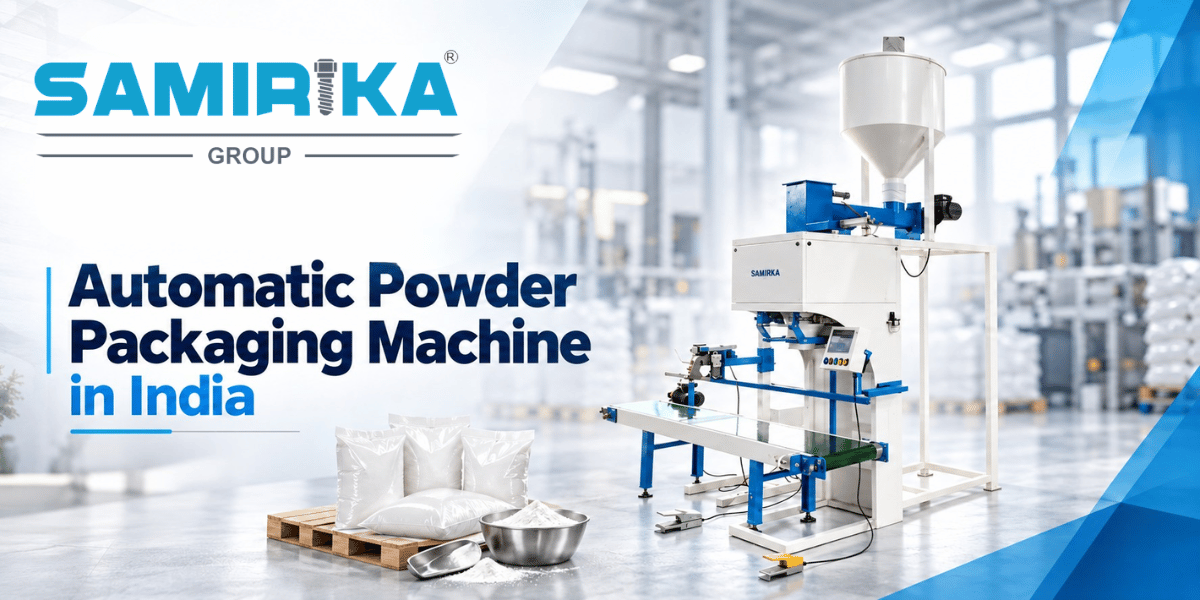
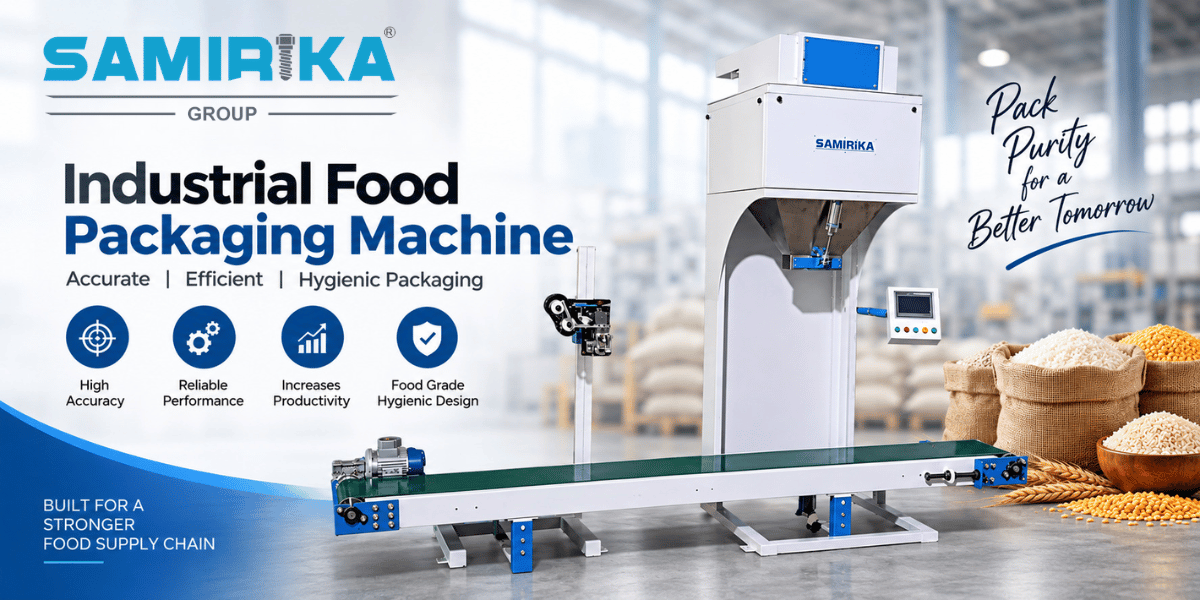
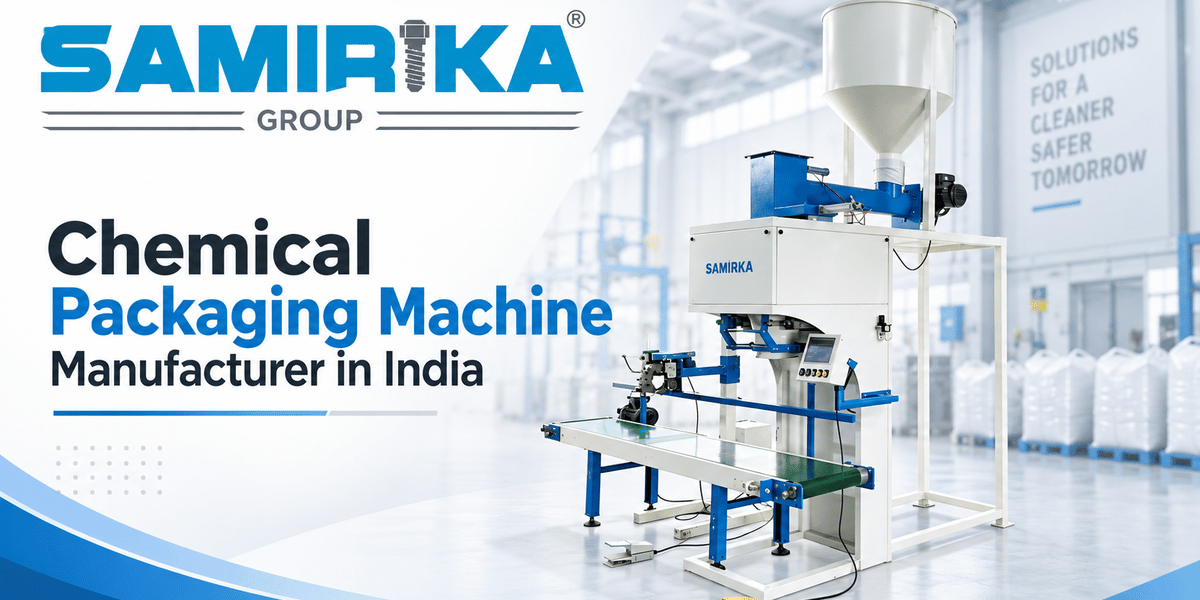
A weighing and bagging machine is a versatile equipment used in various industries for efficient packaging. Its features, benefits, and applications include:
Features:
1. Precision Weighing: Ensures accurate measurement of products for consistent packaging.
2. Conveyor Belt: Moves products from the hopper to the bagging area, streamlining the process.
3. PLC Control System: Offers programmable settings for different products and packaging requirements.
4. Touchscreen Interface: User-friendly controls for easy operation and adjustments.
5. Bag Clamping Mechanism: Secures the bag during filling to prevent spillage.
6. Dust Collection System: Keeps the environment clean by capturing excess dust during bagging.
Benefits:
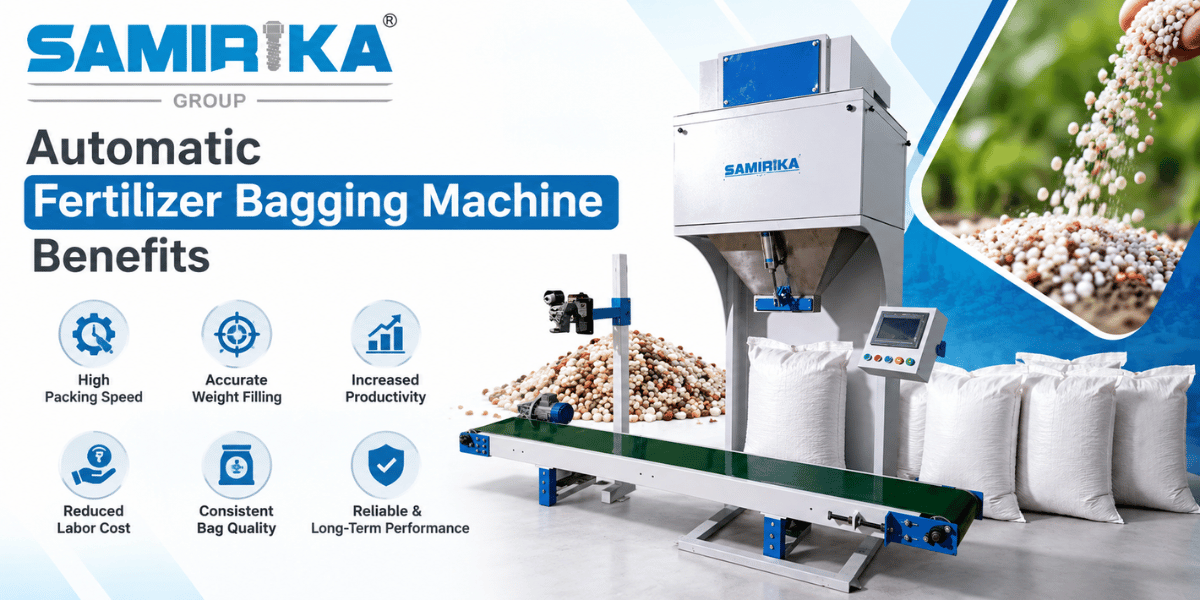
1. Increased Efficiency: Speeds up packaging operations, reducing labor costs and improving productivity.
2. Cost Savings: Minimizes material waste and optimizes bag usage, leading to cost-effective packaging.
3. Consistent Packaging: Ensures each bag contains the same weight, maintaining product quality and customer satisfaction.
4. Improved Safety: Automation reduces manual handling risks, promoting a safer work environment.
5. Versatility: Can handle a wide range of products, such as grains, seeds, powders, and more.
Applications:
1. Agriculture: Used for packaging seeds, grains, fertilizers, and animal feed.
2. Food Industry: Ideal for packaging rice, pulses, flour, spices, snacks, and frozen foods.
3. Chemicals: Suitable for bagging various chemical products, such as powders and granules.
4. Construction: Used to pack cement, sand, and other construction materials.
5. Pharmaceuticals: Precisely packages pharmaceutical powders and granules.
These machines play a crucial role in enhancing packaging efficiency, reducing human errors, and maintaining product consistency across various industries.
Filter Using Product Tags