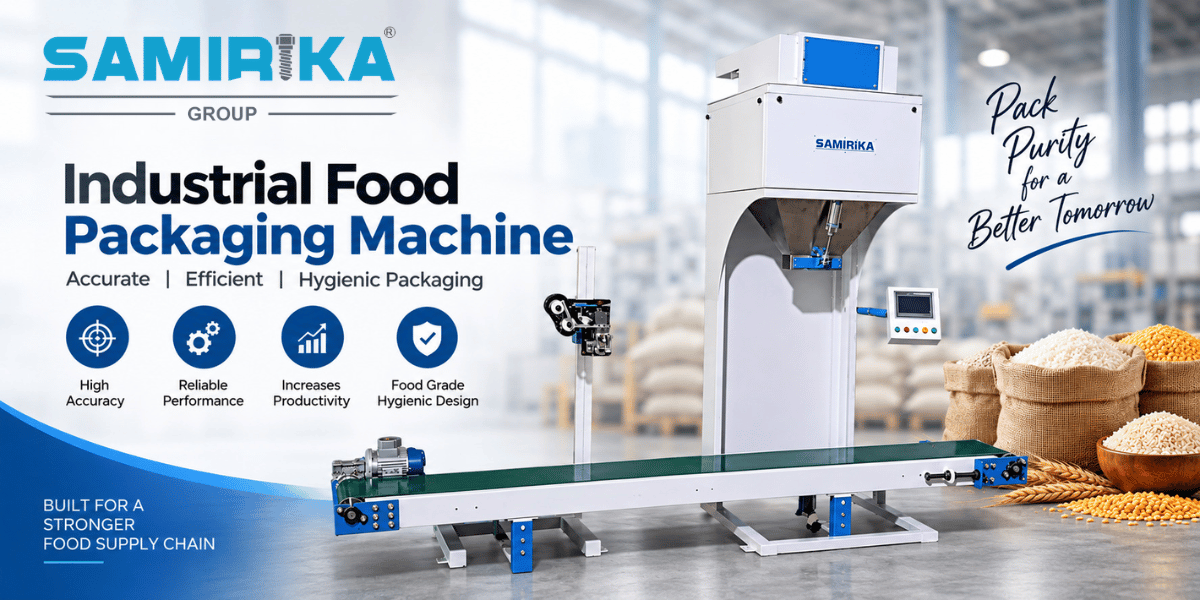
Industrial Food Packaging Machine
In the complex world of food production, the journey from raw ingredients to the consumer's hands involves critical steps, none more vital than packaging. An industrial food packaging machine stands at the forefront of this process, ensuring that products are not only preserved but also presented safely, efficiently, and hygienically. These sophisticated systems are designed to handle a vast array of food items, from delicate powders to granular products, maintaining their integrity while meeting stringent industry standards.
Understanding Industrial Food Packaging Machines
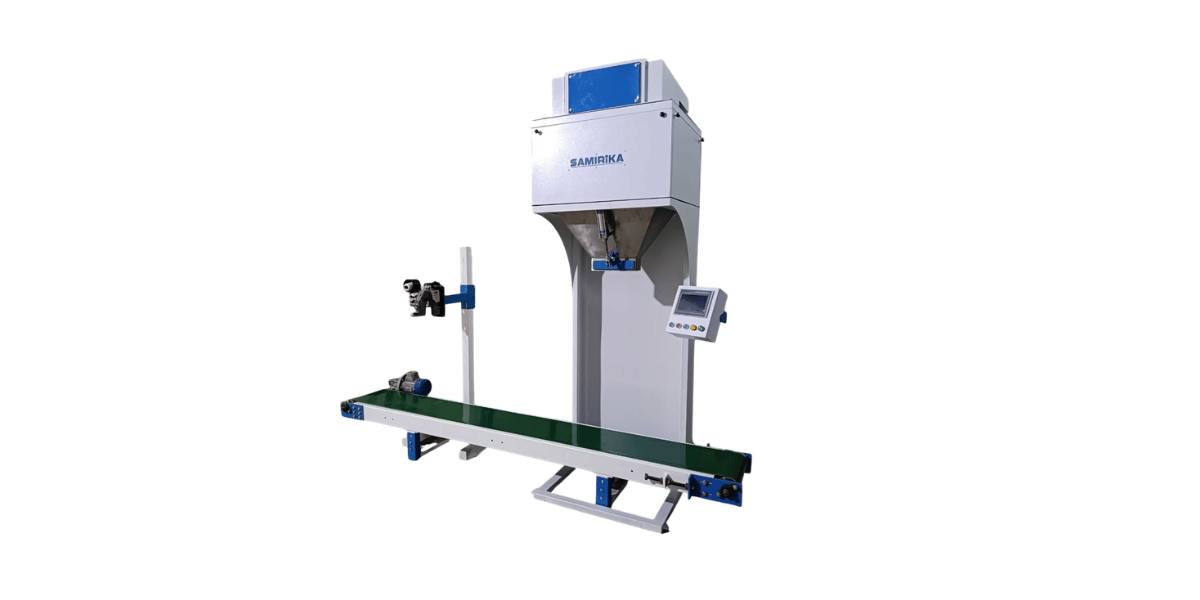
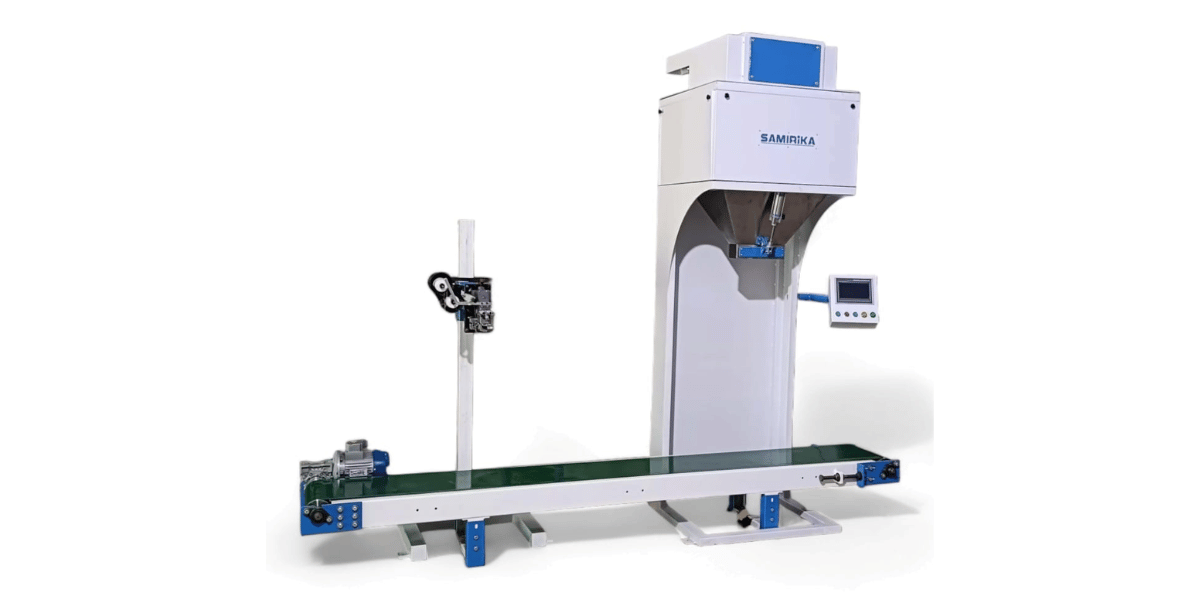
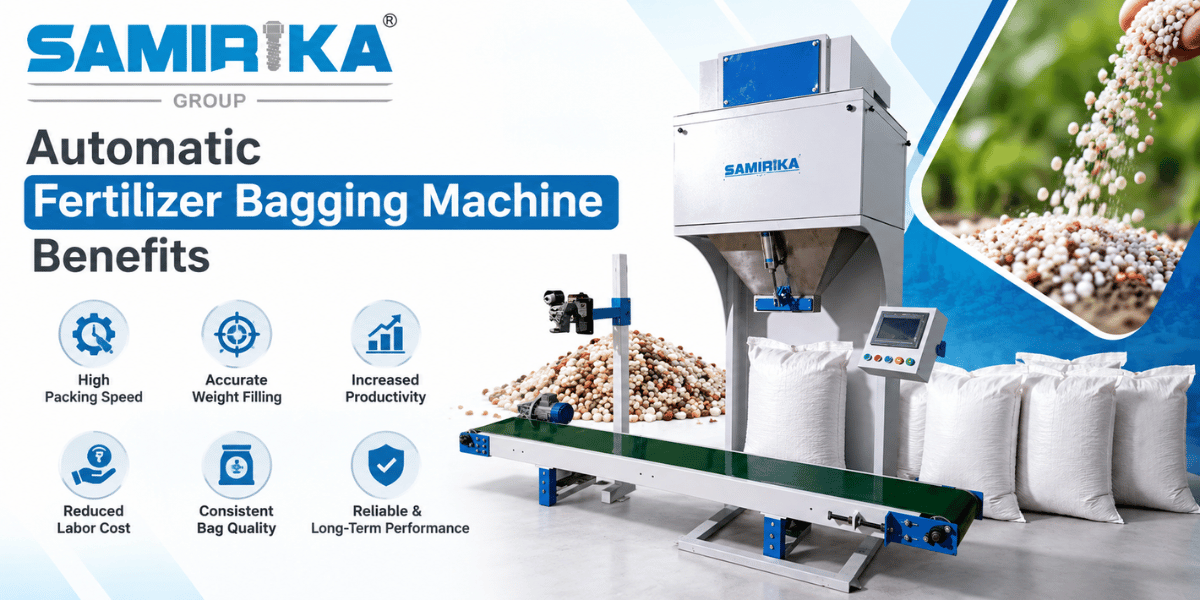
Industrial food packaging machines are specialized pieces of equipment engineered to automate and streamline the process of enclosing food products. Their primary function is to protect food from contamination, spoilage, and physical damage, while also extending shelf life and facilitating distribution. These machines are indispensable for businesses aiming for high-volume production, consistent quality, and operational efficiency.
The food industry demands the highest levels of hygiene and precision. Therefore, food packaging machines are typically constructed with materials that are easy to clean and maintain, often stainless steel, and designed to minimize product contact points. Features such as temperature control, precise filling mechanisms, and airtight sealing capabilities are crucial for preserving the freshness, flavor, and nutritional value of food items.
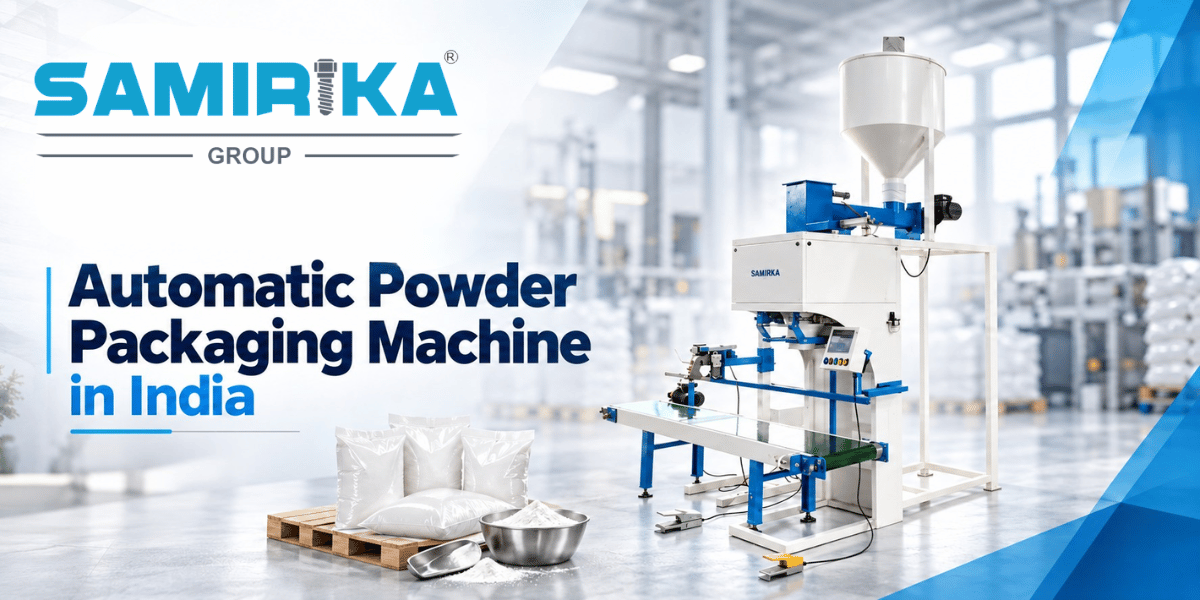
Beyond general food products, specialized machines cater to specific needs. For instance, powder packaging machines are essential for items like flour, spices, sugar, and coffee, requiring systems that can accurately measure and dispense fine particles while managing dust. Similarly, machines for granular products or those needing a robust seal are tailored to their unique handling requirements.
Key Applications in the Food Industry
The versatility of industrial food packaging machines makes them suitable for a broad spectrum of applications across the food sector. Their ability to adapt to different product types and packaging formats is a testament to their advanced engineering.
Agro and Food Packaging
Automated solutions for packaging grains, seeds, pulses, and other agricultural commodities, ensuring accurate weight and secure sealing.
Powder and Granule Packaging
High-speed, accurate weighing and filling systems designed for powders like flour, sugar, spices, and coffee, often with dust control features.
Snack and Confectionery Packaging
Machines that can handle individual items or bulk products, providing attractive and tamper-evident packaging for snacks and sweets.
Dairy and Cheese Products
Specialized packaging that may include vacuum sealing or modified atmosphere packaging (MAP) to preserve the freshness of dairy items and cheeses.
Liquid and Semi-Liquid Food Packaging
While often distinct, some systems can handle viscous liquids or semi-liquids, ensuring precise filling and secure closure.
Advantages of Modern Food Packaging Machinery
Implementing advanced industrial food packaging machines offers significant advantages that contribute to a company's overall success and market competitiveness.
- Enhanced Product Safety & Quality: Minimizes contamination risks and preserves product integrity through hygienic design and precise packaging.
- Increased Production Efficiency: Automation significantly speeds up the packaging process, allowing for higher output volumes.
- Reduced Operational Costs: Automation lowers labor requirements and minimizes product waste due to accurate filling and sealing.
- Consistent Packaging: Ensures uniform package appearance and seal integrity, which is crucial for brand consistency and consumer trust.
- Extended Shelf Life: Effective sealing and protective packaging help maintain product freshness for longer periods, reducing spoilage.
- Compliance with Regulations: Modern machines are designed to meet strict food safety and hygiene standards.
Choosing the Right Industrial Food Packaging Machine
Selecting the appropriate industrial food packaging machine is a critical decision that requires careful consideration of various factors. Samirika Group understands the unique challenges faced by food manufacturers and offers solutions designed for performance and reliability.
Buyer Insight: Focus on Hygiene and Precision
When evaluating food packaging machinery, prioritize ease of cleaning and sanitization. Look for designs that minimize crevices where bacteria can harbor. Precision in filling and sealing is also paramount to prevent product loss and ensure consumer satisfaction.
Key Selection Criteria:
- Product Type: Is it a powder, granular, liquid, solid, or semi-liquid product? Different machines are optimized for different forms.
- Packaging Material: What type of bags or containers will be used? Consider material compatibility for sealing.
- Required Throughput: How many packages per minute or hour do you need to produce?
- Accuracy Requirements: Precise weighing and filling are essential to avoid over- or under-filling.
- Hygiene Standards: Ensure the machine meets food-grade requirements and is easy to clean.
- Automation Level: Determine the desired level of automation, from semi-automatic to fully integrated systems.
- Space and Integration: Consider the available factory space and how the machine will integrate with existing production lines.
Quality Checks Before Purchase:
- Material Construction: Verify that food-grade materials like stainless steel are used where appropriate.
- Seal Integrity: Ensure the machine produces strong, airtight, and leak-proof seals.
- Weighing Accuracy: If applicable, confirm the accuracy and repeatability of the weighing system.
- Ease of Operation & Maintenance: The machine should be user-friendly and easy to maintain.
- Dust Control: For powder packaging, effective dust containment is crucial for workplace safety and product loss reduction.
Questions to Ask Your Supplier:
- Can the machine handle my specific product characteristics (e.g., stickiness, flowability, particle size)?
- What is the typical accuracy of the filling and weighing system?
- What types of packaging materials can be used with this machine?
- How easy is it to change over between different product sizes or packaging types?
- What are the cleaning and maintenance procedures?
- Does the machine include dust collection or control features?
Samirika Group: Your Partner in Packaging Automation
Samirika Group specializes in providing robust material handling and automated packaging solutions tailored to the diverse needs of the food industry. Our expertise extends to a wide range of machinery designed for efficiency, accuracy, and reliability.
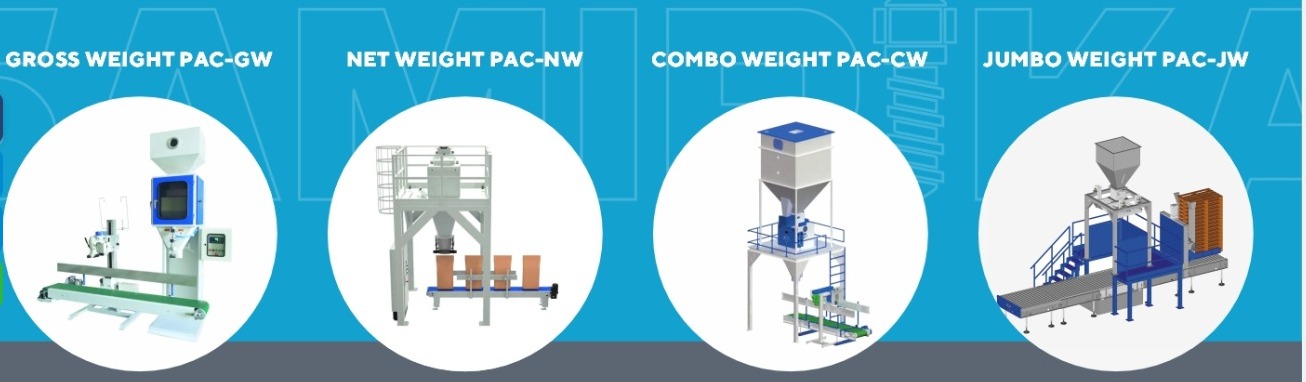
We offer specialized solutions including advanced Industrial Food Packaging Machines, precise weighing and bagging systems, and efficient conveying systems. For specific food product needs, our Agro and Food Packaging Machines ensure optimal handling and secure packaging. If your products involve powders, our Chemical and Hygienic Powder Packaging Machines are designed with dust control and accuracy in mind. We also provide Bag Heat Sealing Machines that create strong, airtight seals crucial for preserving food freshness and integrity.
Our commitment is to enhance your production capabilities with integrated automation. By understanding your unique operational challenges, we can recommend and implement the most suitable packaging and material handling systems to optimize your processes.
Frequently Asked Questions
What makes an industrial food packaging machine different from a general packaging machine?
Industrial food packaging machines are specifically designed with food safety, hygiene, and product integrity as top priorities. They often feature stainless steel construction, easy-to-clean designs, and precise filling and sealing mechanisms to meet stringent food industry regulations and prevent contamination.
Can a single machine handle both powders and granules?
Some versatile machines can handle both, but often the optimal design differs. Machines designed for powders focus on accurate volumetric or gravimetric filling and dust control, while those for granules might prioritize gentle handling to prevent breakage and ensure consistent flow.
What is the importance of airtight sealing in food packaging?
Airtight sealing is crucial for preventing spoilage by keeping out oxygen, moisture, and contaminants. It helps maintain product freshness, extends shelf life, and preserves flavor and nutritional value. For certain products, it also ensures tamper evidence.
How does dust control benefit food powder packaging?
Dust control is vital for worker safety (preventing inhalation), environmental cleanliness on the factory floor, and product integrity (preventing loss and contamination). It ensures a safer and more efficient packaging operation.
Optimize Your Food Packaging Process
Ready to enhance your production efficiency, ensure product safety, and achieve superior packaging quality? Explore the advanced industrial food packaging machine solutions offered by Samirika Group. Contact us to discuss your specific requirements and find the automation solution that best fits your business needs.
Request a Consultation