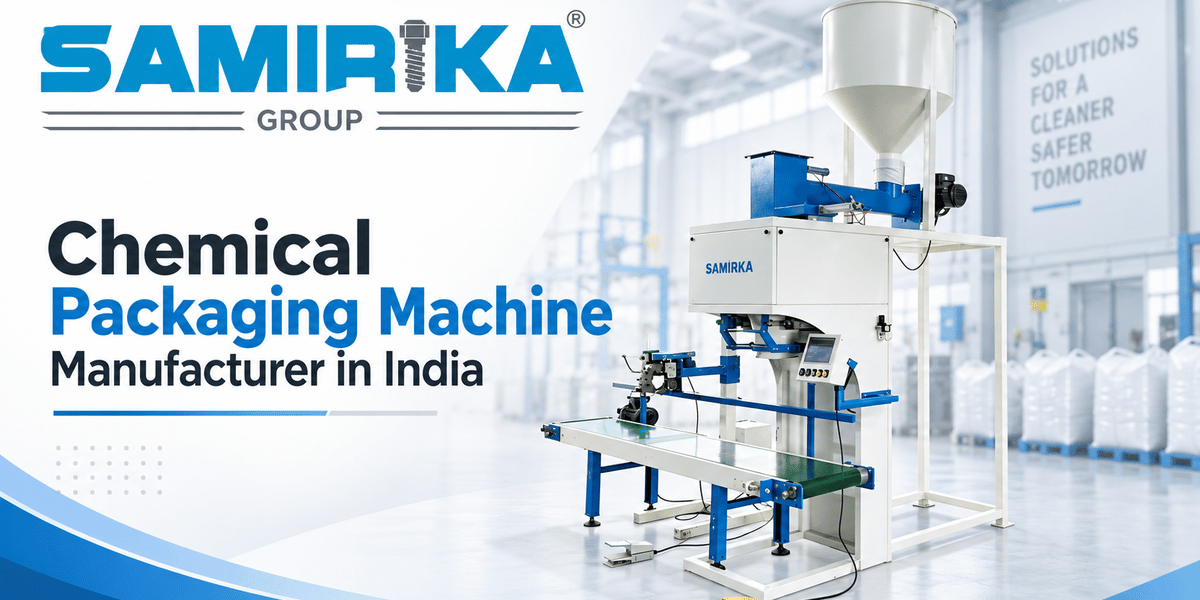
Chemical Packaging Machine Manufacturer in India
The chemical industry demands precision, safety, and efficiency in every aspect of its operations, especially when it comes to packaging. Handling diverse chemical products, from fine powders to granular substances, requires specialized machinery that can ensure product integrity, prevent contamination, and comply with stringent safety regulations. As a pivotal hub for industrial manufacturing, India hosts several key players in the packaging machinery sector. Among these, Samirika Industries stands out as a dedicated manufacturer of chemical packaging machines, offering a comprehensive range of automated solutions designed to meet the rigorous demands of this sector.
This guide delves into the critical role of chemical packaging machines, exploring their applications, the benefits of automation, and the essential factors to consider when selecting a reliable manufacturer in India. We will highlight how advanced packaging technology can optimize operations, enhance product safety, and contribute to a more sustainable and efficient supply chain for chemical producers.
Understanding Chemical Packaging Machines
Chemical packaging machines are specialized pieces of equipment engineered to fill, seal, and sometimes palletize various chemical products. The complexity and type of machinery required depend heavily on the physical properties of the chemical being packaged – whether it's a fine powder, granules, viscous liquid, or solid. The primary goals of these machines are to ensure accurate dosing, maintain product purity, prevent leaks, protect the product from environmental factors, and guarantee the safety of both the product and the handling personnel.
In India, the demand for sophisticated chemical packaging solutions has surged due to the growth of the chemical sector, increased focus on automation, and stricter regulatory environments. Manufacturers like Samirika Industries are at the forefront, developing machines that incorporate advanced control systems, robust construction, and user-friendly interfaces.
Key Applications and Use Cases in the Chemical Industry
Chemical packaging machines are versatile and find applications across numerous sub-sectors within the chemical industry:
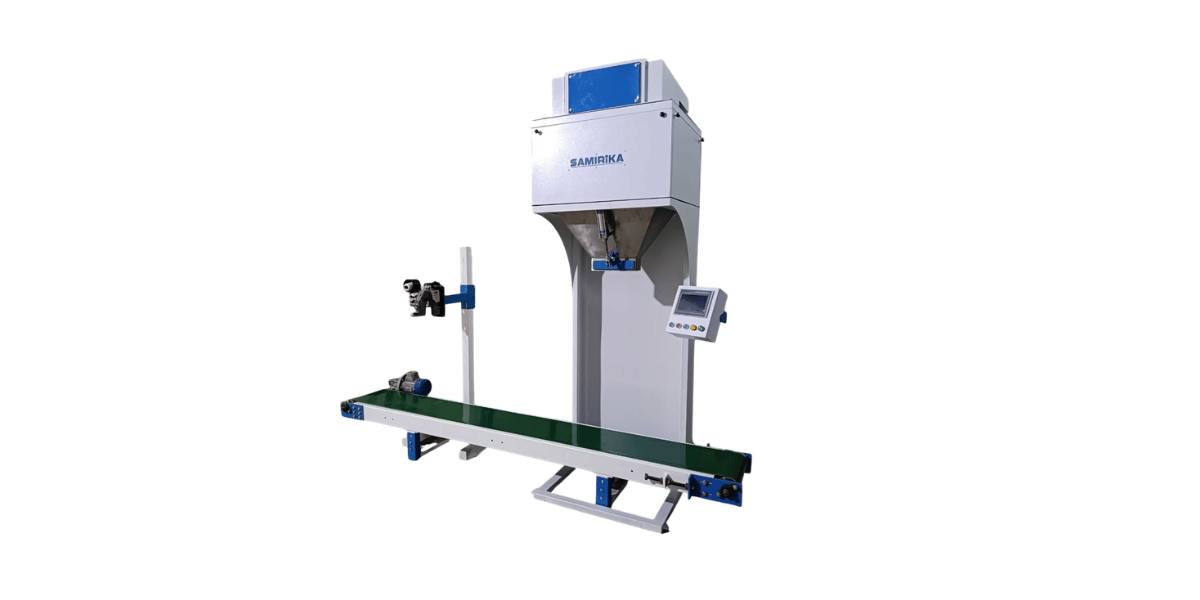
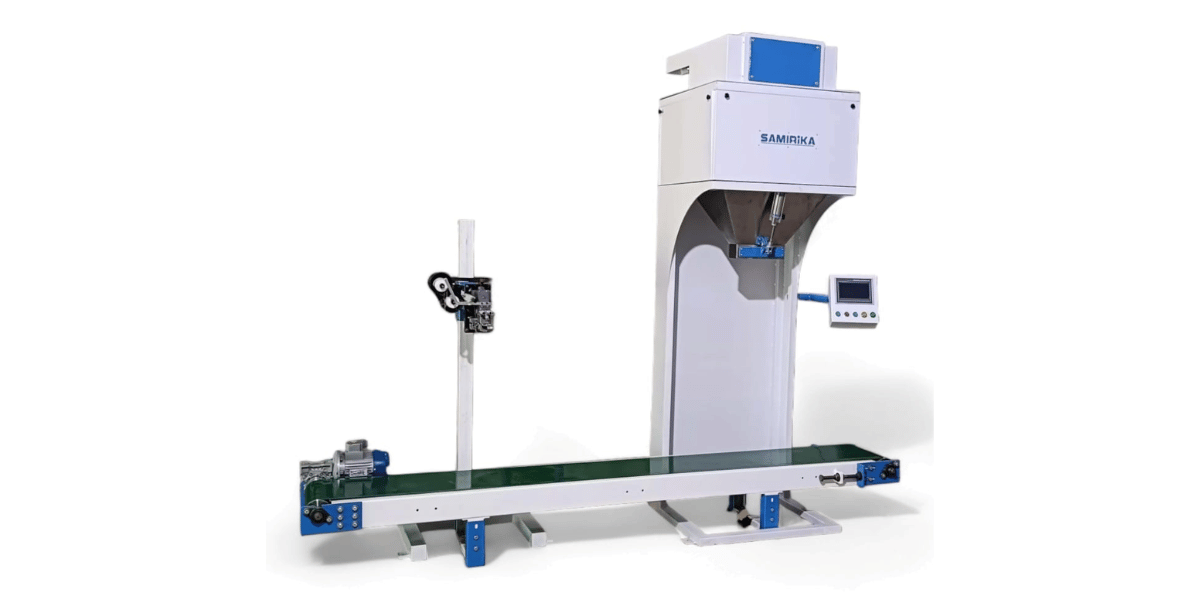
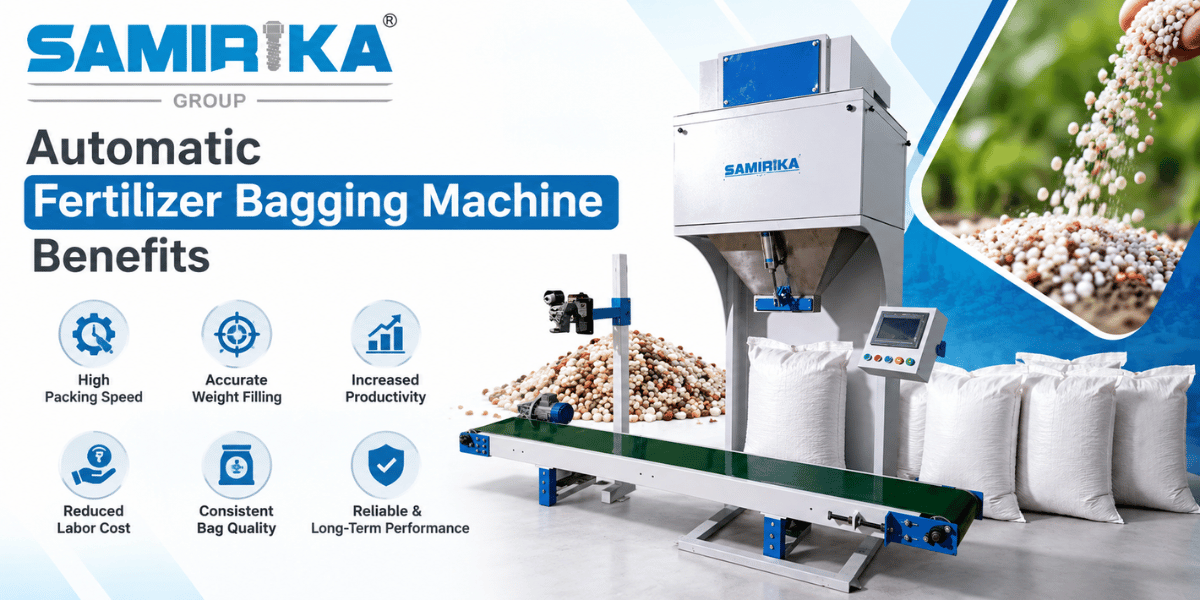
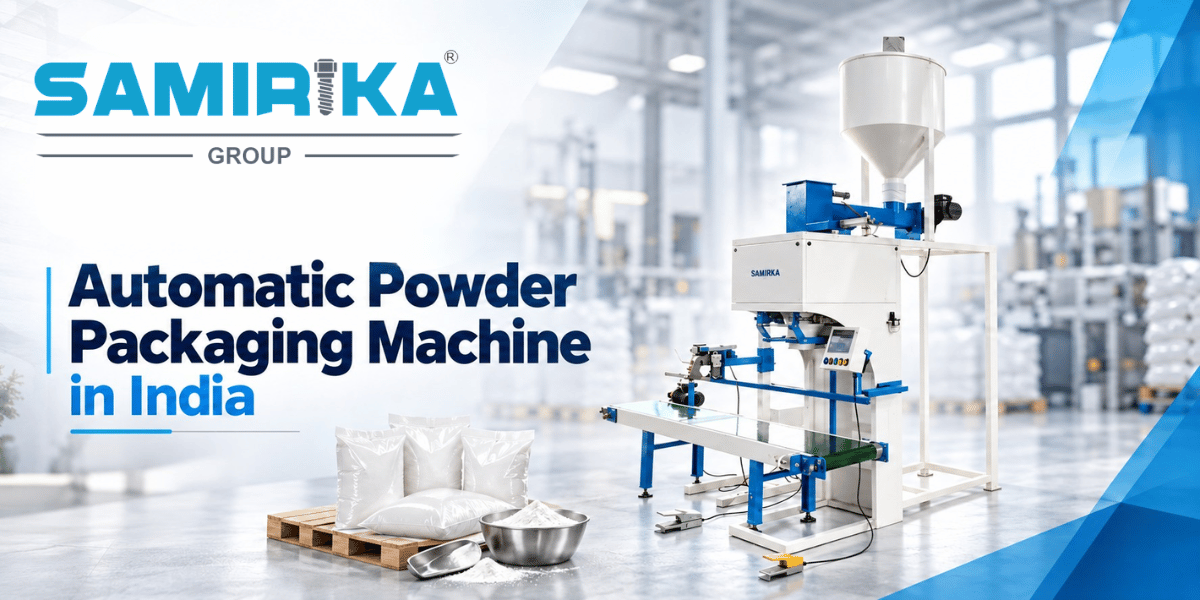
- Powder and Granule Packaging: Machines designed for fine powders and granular chemicals ensure precise filling into bags, drums, or intermediate bulk containers (IBCs), preventing dust release and ensuring accurate weight. This includes products like fertilizers, pigments, plastic resins, and chemical additives.
- Polymer Packaging: Specialized systems handle the unique challenges of packaging polymers, often in pellet or granular form, into various sizes of bags or containers.
- Jumbo Bag (FIBC) Filling: For bulk chemicals, large Flexible Intermediate Bulk Containers (FIBCs), often called jumbo bags or bulk bags, are filled efficiently using dedicated machines that ensure proper positioning and filling of the container.
- Liquid and Paste Packaging: While this article focuses on solid chemical packaging, some manufacturers offer solutions for viscous liquids or pastes, requiring different filling and sealing mechanisms.
- Specialty Chemicals: Packaging for hazardous or high-value specialty chemicals often requires enhanced containment, inert atmosphere capabilities, and tamper-evident sealing to ensure safety and product integrity.
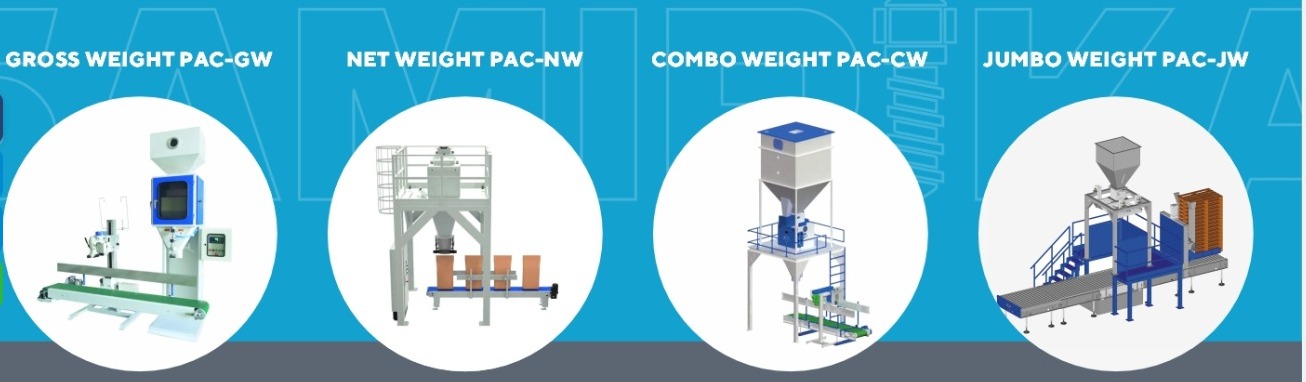
Samirika Industries offers a comprehensive suite of solutions, including specialized options for