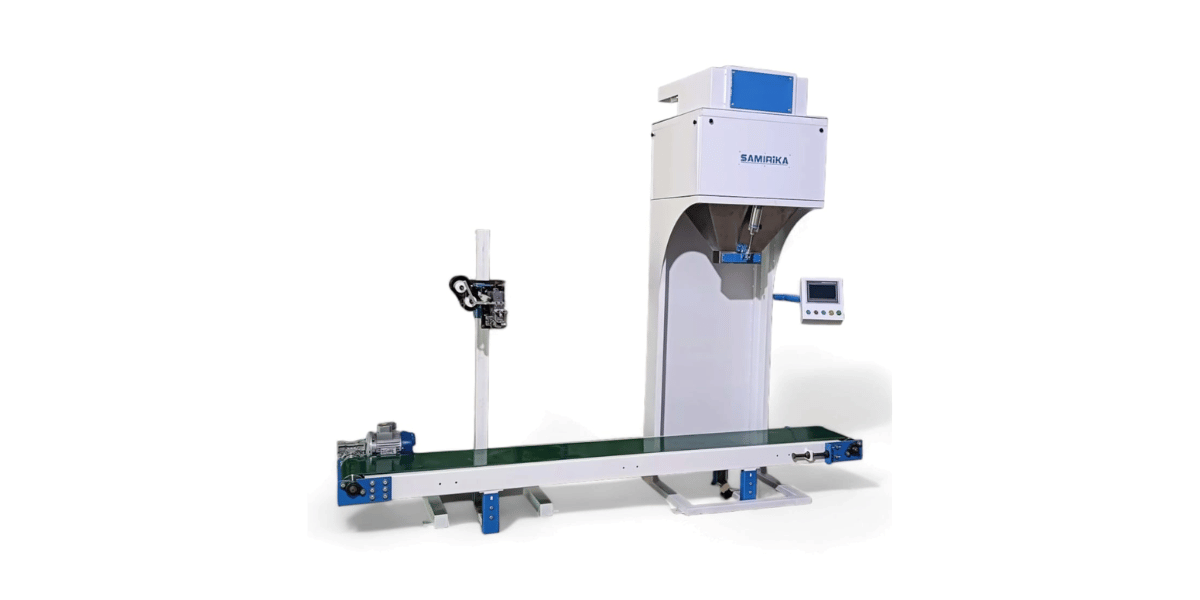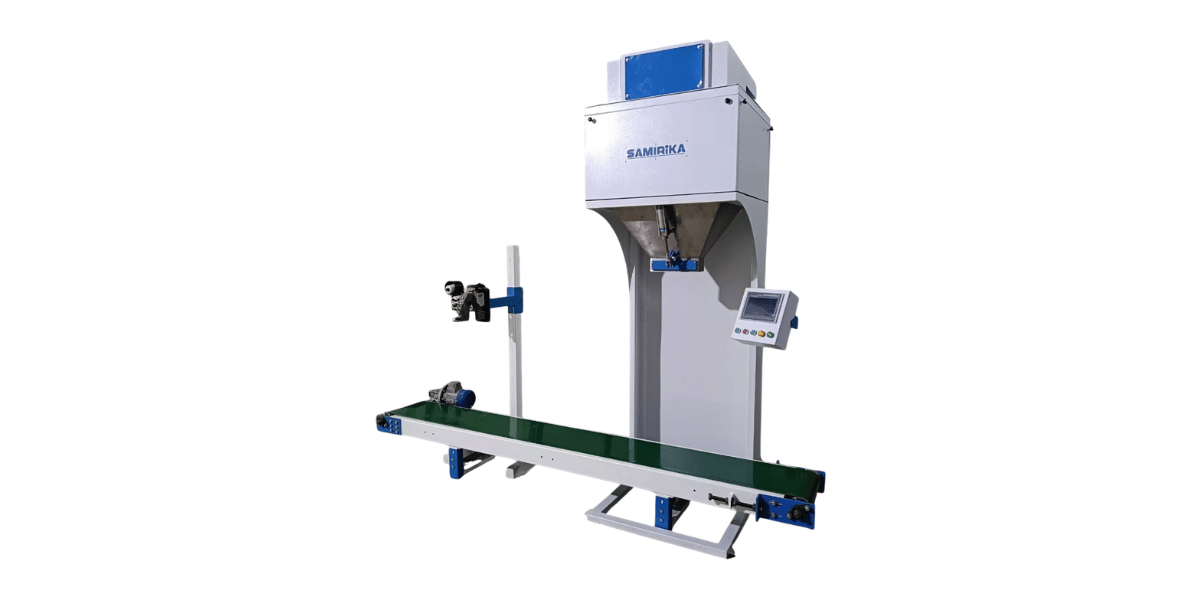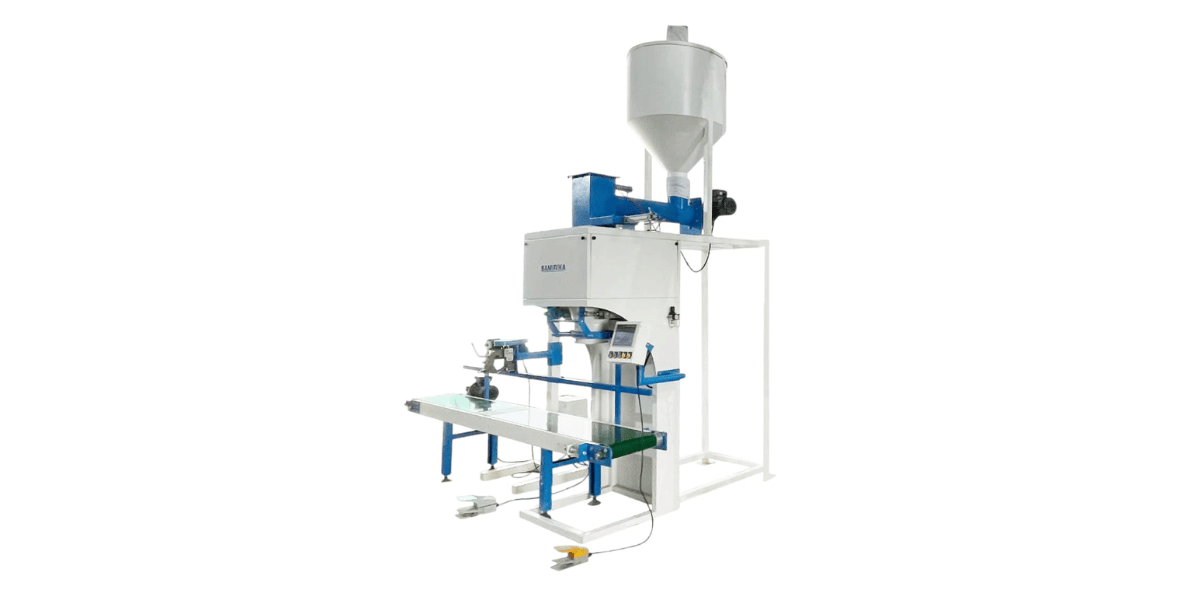
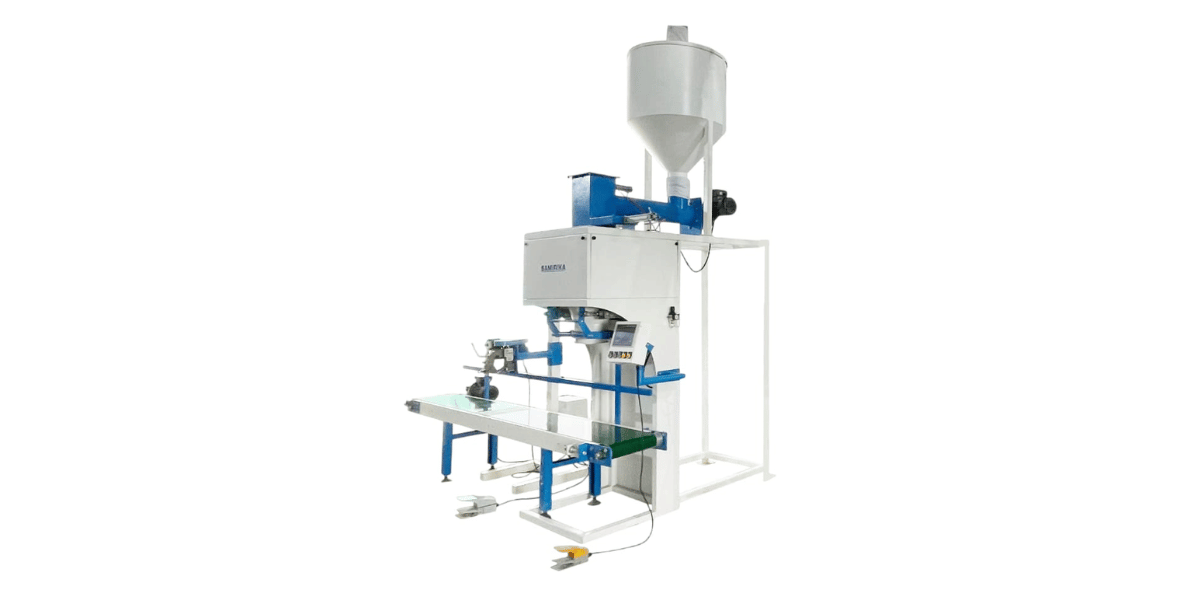
Powder Packing Machine for Chemical Industry
The chemical industry relies heavily on precision, safety, and efficiency in every stage of its operations. Packaging is a critical final step, demanding specialized equipment capable of handling diverse chemical powders with accuracy and security. A high-quality powder packing machine designed for the chemical industry is not just a piece of equipment; it's a crucial component that ensures product integrity, operator safety, and streamlined production. Samirika Industries provides advanced solutions tailored to meet the stringent demands of chemical powder packaging.
Understanding Chemical Powder Packing Machines
A powder packing machine for the chemical industry is a sophisticated piece of machinery engineered to precisely fill and seal various types of chemical powders into bags or containers. These systems are integral to operations that require accurate measurement, safe handling, and secure containment of powdered substances, which can range from fine dusts to granular materials.
The core function of these machines involves controlled dispensing of the powder, precise weighing to ensure each package meets specific weight requirements, and robust sealing to prevent spillage, contamination, or degradation of the product. Modern machines are designed with automation in mind, minimizing manual intervention and enhancing throughput while maintaining high standards of accuracy and safety. This is particularly vital in the chemical sector where even minor deviations can have significant consequences.
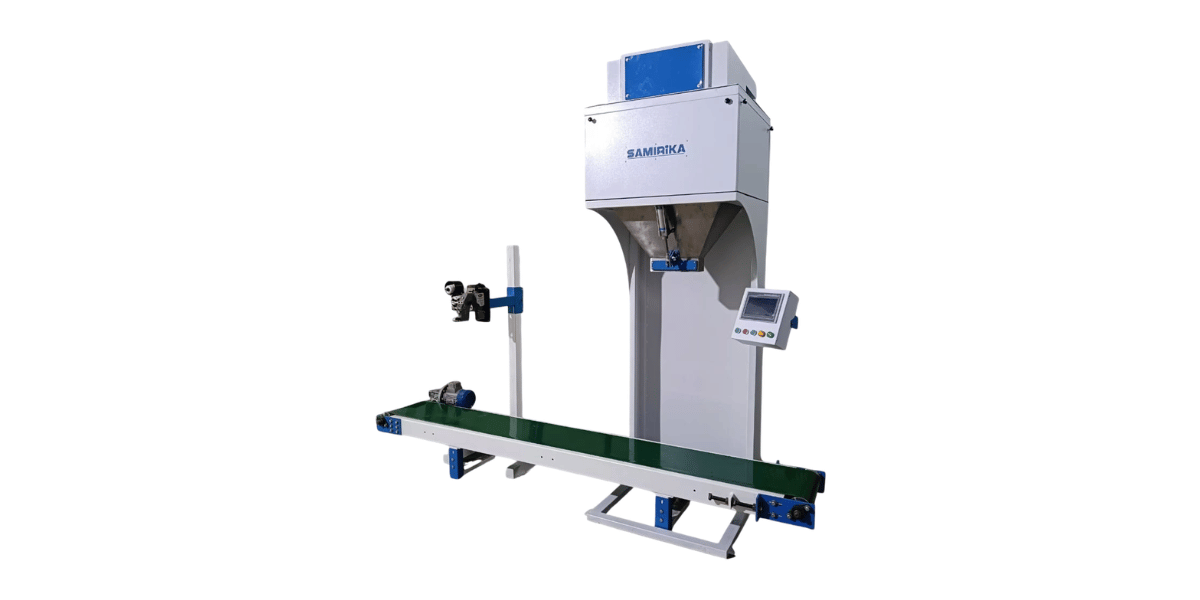
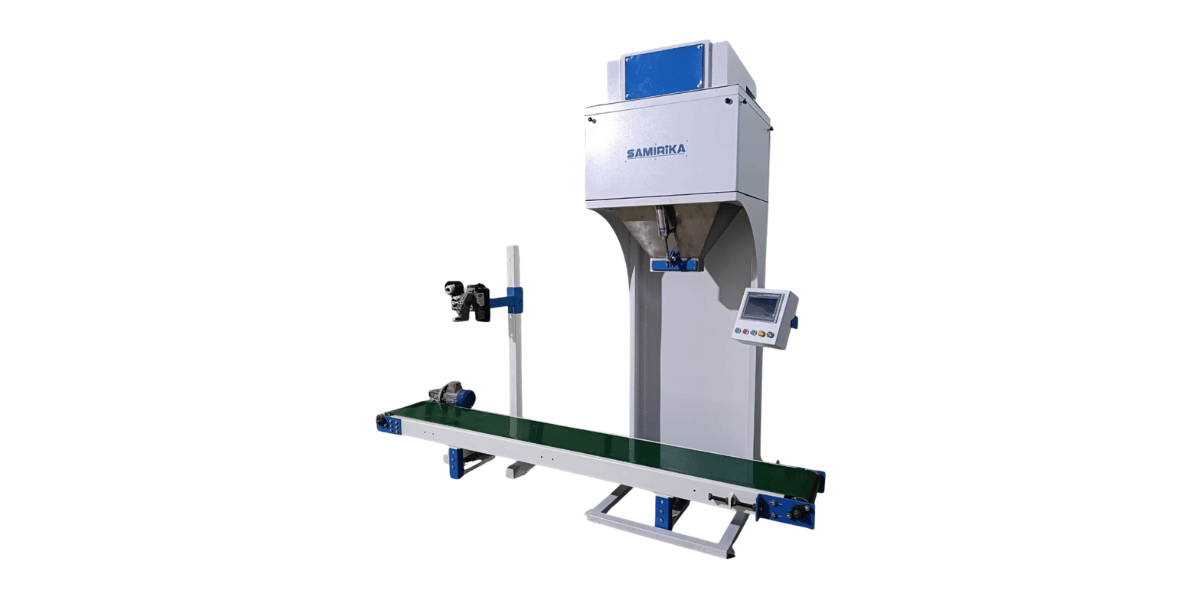
Samirika Industries offers a range of solutions, including specialized Chemical and Hygienic Powder Packaging Machines, designed to cater to the unique challenges presented by chemical powders. Their Semi Automatic Chemical Powder Packing Machine, for instance, is built for free-flowing materials and can handle capacities of up to 250 bags per hour, specifically designed for open-mouth bags. This highlights their commitment to providing tailored solutions for specific industrial needs.
Applications in the Chemical Sector
The versatility of powder packing machines makes them indispensable across numerous applications within the chemical industry:
Specialty Chemicals
Packaging fine chemical powders, reagents, catalysts, and additives where precise dosing and containment are paramount.
Pharmaceutical Ingredients
Handling active pharmaceutical ingredients (APIs) and excipients, requiring hygienic conditions and extremely accurate filling to meet strict regulatory standards.
Agrochemicals
Packaging fertilizers, pesticides, herbicides, and other agricultural chemicals, often in larger bags, ensuring product stability and safety during handling and application.
Dyes and Pigments
Filling colorants and pigments where dust control is essential to maintain a clean working environment and prevent cross-contamination.
Household Chemicals
Packaging detergents, cleaning powders, and other household chemical products into various bag sizes.
Water Treatment Chemicals
Packing powdered chemicals used for water purification and treatment processes, ensuring they remain free from moisture and contaminants.
Key Features and Practical Benefits
Modern powder packing machines for the chemical industry are equipped with advanced features that translate into significant operational benefits:
Core Components and Functionality
- Accurate Weighing Systems: Utilize gravimetric or volumetric dosing, such as auger fillers for precision with non-free-flowing powders or basculating dosing for high-speed free-flowing materials. This ensures precise product quantity in every bag, reducing material waste and meeting customer expectations.
- Reliable Feeding Mechanisms: Consistent material flow from hoppers to the filling system is managed through robust designs that prevent bridging or clogging, ensuring uninterrupted operation.
- Flexible Packaging Options: Machines can handle various bag sizes, types (pillow, gusseted), and materials, adapting to different product needs and market demands.
- Dust Collection Systems: Integrated systems capture airborne powder during filling and sealing, promoting a cleaner, safer working environment and minimizing product loss.
- Intuitive Control Panels: User-friendly interfaces allow for easy operation, setting of parameters, and monitoring of the packing process.
- Safety Features: Incorporate emergency stop buttons, safety interlocks, and robust construction to protect operators and prevent accidents.
Performance Advantages
- Enhanced Productivity: High-speed capabilities and automation reduce labor requirements and increase output, leading to greater overall efficiency.
- Product Integrity: Secure sealing prevents contamination, moisture ingress, and spillage, preserving the quality and shelf-life of chemical products.
- Operational Safety: Minimized manual handling and dust control features significantly improve workplace safety for personnel.
- Cost Efficiency: Precise filling reduces material waste, while automation lowers labor costs, contributing to a better return on investment.
- Compliance: Machines designed for hygienic or contamination-free operation can help meet industry regulations.
Selecting the Right Powder Packing Machine
Choosing the appropriate powder packing machine is crucial for optimizing your chemical packaging operations. Consider the following factors:
Key Selection Criteria
- Product Characteristics: Evaluate the powder's flowability (free-flowing vs. non-free-flowing), particle size, density, abrasiveness, and any sensitivity to heat or moisture. This determines the most suitable dosing mechanism (auger, basculating, etc.).
- Bag Type and Size: Determine the required bag dimensions, material (e.g., multi-wall paper, plastic, woven PP), and style (pillow, gusseted, open-mouth).
- Required Capacity: Assess your production volume needs. Machines vary in speed, from semi-automatic options like Samirika's 250 Bags/Hour model to fully automated, high-speed systems.
- Accuracy Requirements: Consider the tolerance for weight variation. High-accuracy dosing systems are essential for valuable or regulated chemical products.
- Environmental Considerations: Does the application require dust collection? Are there specific hygiene standards to meet? Some machines feature contamination-free designs and robust dust extraction.
- Integration Needs: Will the packing machine need to integrate with existing or future equipment such as conveyors, check weighers, bag sealers, or palletizers?
- Automation Level: Decide between semi-automatic (requiring some manual intervention) and fully automatic systems based on labor availability, budget, and desired throughput.
Buyer Insight: When dealing with potentially corrosive chemical products, inquire about specialized sealing blocks, such as those made from titanium and carbon, which offer enhanced durability and resistance.
Questions to Ask Before Purchasing
- What is the most accurate and efficient dosing method for my specific powder?
- Can the machine handle the range of bag sizes and types I intend to use?
- What is the guaranteed throughput and accuracy under real-world operating conditions?
- What maintenance is required, and what is the availability of spare parts?
- Does the machine incorporate adequate safety features and dust control measures?
- Can the system be integrated with my existing production line?
Samirika Industries: Your Partner in Chemical Packaging
Samirika Industries Pvt. Ltd. is dedicated to providing comprehensive material handling and automation systems, including specialized solutions for the chemical industry. Established with a vision to deliver quality and efficiency, the company offers a complete range of products designed to streamline packaging processes.
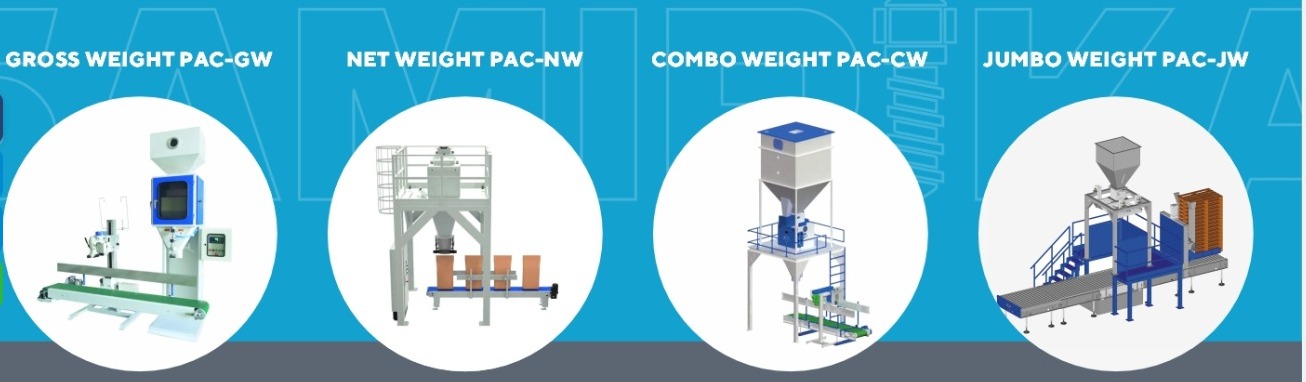
Their offerings include advanced automatic weighing and bagging systems, polymer packaging machines, and jumbo packing machines, all equipped with microprocessor-based controllers for precise operation. For the chemical sector, Samirika provides robust Chemical and Hygienic Powder Packaging Machines, ensuring accurate filling, weighing, and sealing. Their commitment extends to providing reliable systems like the Semi Automatic Chemical Powder Packing Machine, capable of handling up to 250 bags per hour for free-flowing and chemical powders into open-mouth bags.
Located in Ahmedabad, Gujarat, Samirika Industries focuses on delivering automation solutions that enhance productivity, safety, and reliability for its clients. They strive to be a dependable partner, offering tailored equipment to meet the evolving needs of the chemical industry.
Frequently Asked Questions
What types of chemical powders can these machines handle?
These machines are designed to handle a wide range of chemical powders, including free-flowing materials, non-free-flowing powders, fine dusts, and granular substances. The specific type of dosing system (e.g., auger, basculating) will be chosen based on the powder's characteristics.
How is accuracy ensured in chemical powder packaging?
Accuracy is achieved through sophisticated weighing systems, such as gravimetric or volumetric fillers, which precisely measure the powder before it's filled into the bag. Advanced machines may also include under-overweight rejection systems.
Are dust control measures included in these machines?
Yes, many chemical powder packing machines are equipped with integrated dust collection or extraction systems to maintain a clean working environment, improve safety, and minimize product loss.
What level of automation is available?
Both semi-automatic and fully automatic powder packing machines are available. Semi-automatic options require some manual intervention, while fully automatic systems handle the entire process from bag filling to sealing with minimal operator involvement.
Can these machines handle corrosive chemical products?
For corrosive products, specific configurations may be required, such as specialized sealing blocks made from materials like titanium and carbon, which offer enhanced resistance.
Optimize Your Chemical Packaging Process Today
Invest in a powder packing machine that ensures precision, safety, and efficiency for your chemical products. Samirika Industries offers reliable, automated solutions tailored to the specific demands of the chemical industry.
Contact Samirika Industries to discuss your requirements and get a customized packaging solution.