Powder Packaging Machine for Chemical Industry
The chemical industry demands unparalleled precision, safety, and reliability in every operational aspect, and powder packaging is no exception. Handling fine powders, granular materials, and hazardous substances requires specialized equipment designed to maintain product integrity, protect personnel, and ensure environmental compliance. An advanced powder packaging machine is not merely a tool for containment; it's a critical component of a safe and efficient chemical supply chain. Samirika Group offers comprehensive material handling systems, including sophisticated solutions tailored for the unique challenges of chemical powder packaging.
What Are Powder Packaging Machines for the Chemical Industry?
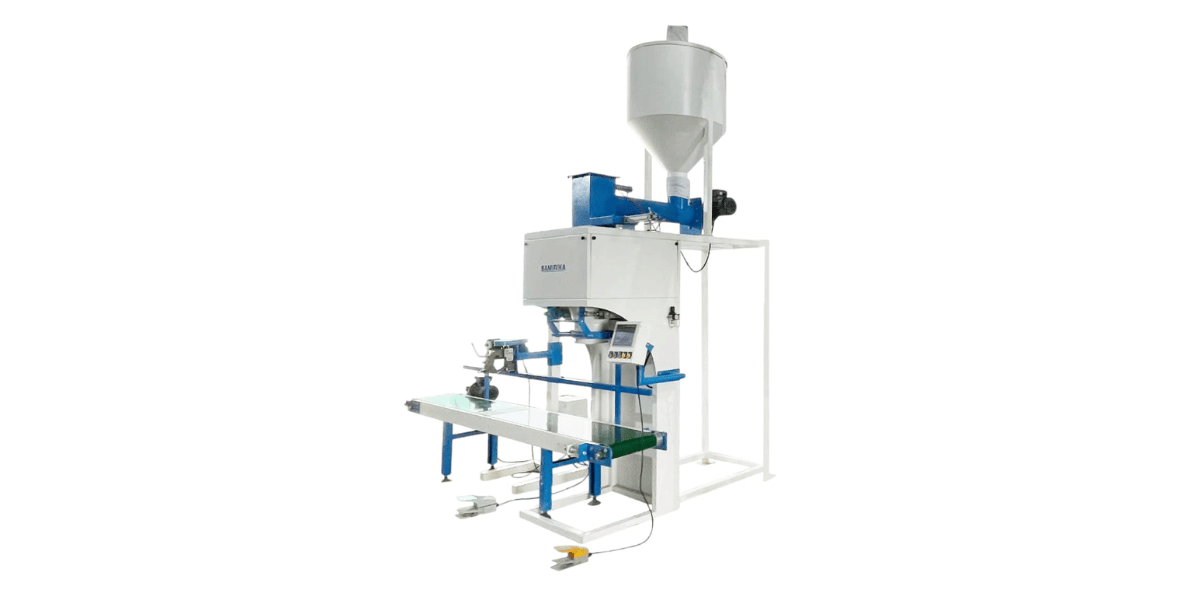
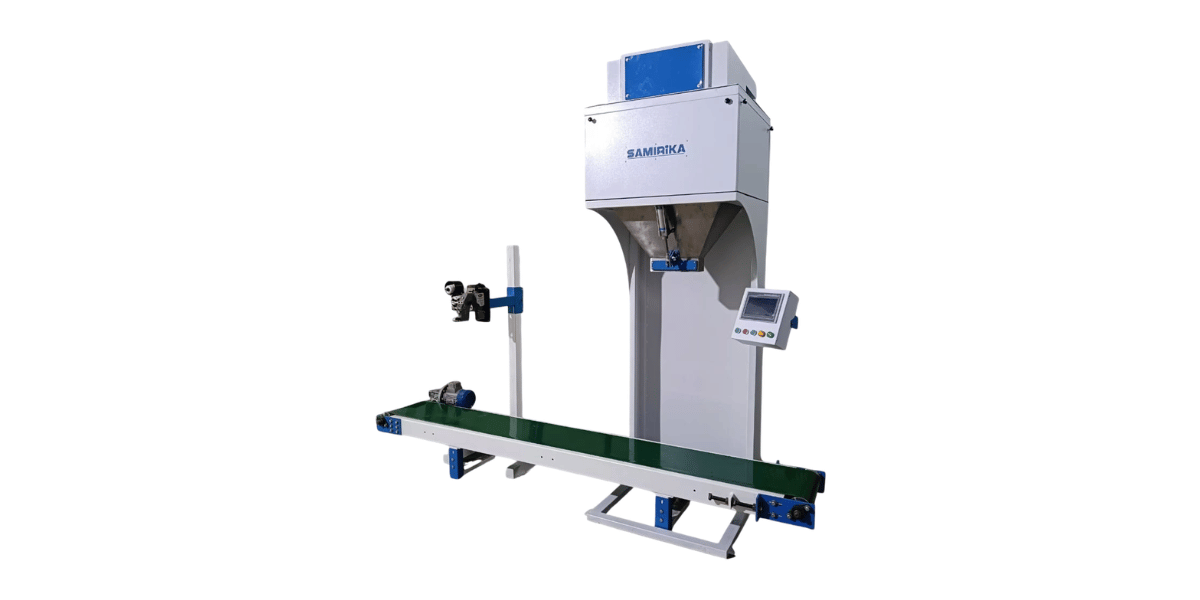
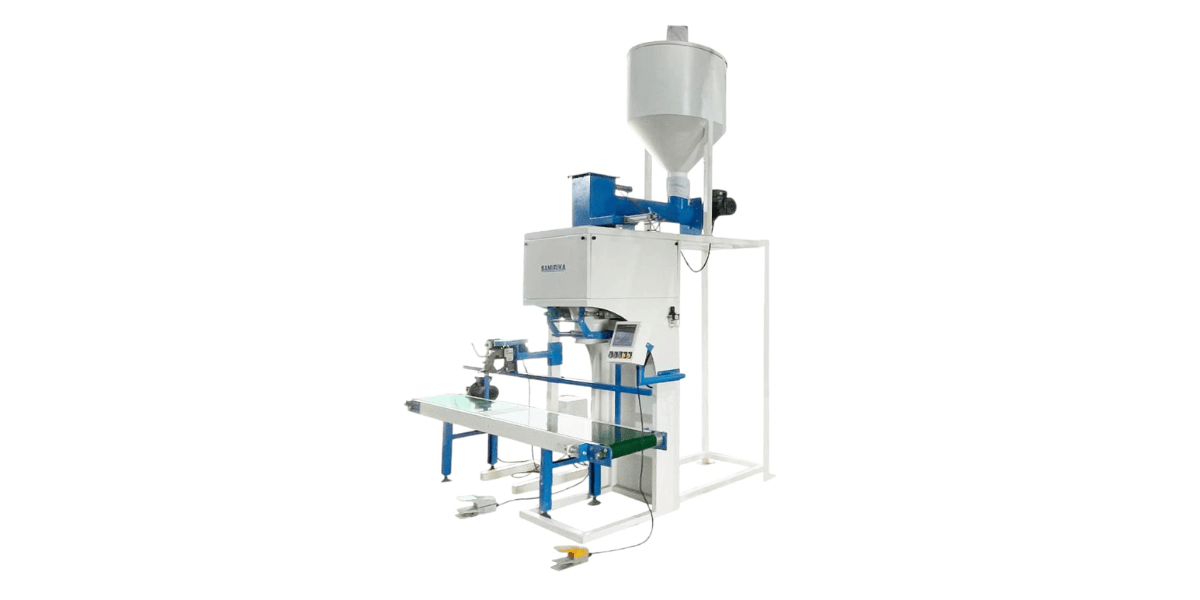
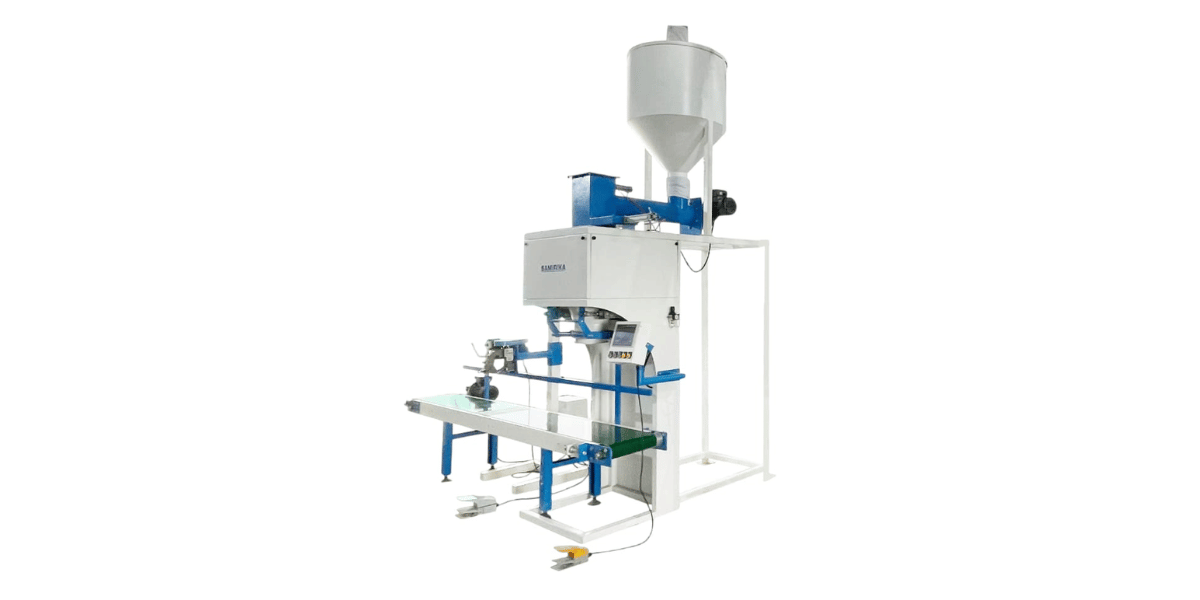
Powder packaging machines designed for the chemical industry are highly specialized automated systems engineered to accurately fill, weigh, and seal various types of chemical powders into bags, sacks, or other containers. These machines are built with materials and features that can withstand potentially corrosive or abrasive substances, ensure dust containment, and provide precise volumetric or gravimetric filling to meet stringent industry standards. Their primary function is to automate the often complex and hazardous process of packaging chemical products, transforming raw materials into ready-to-distribute goods while maintaining safety and product quality.
These systems are integral to operations involving fertilizers, pigments, dyes, industrial chemicals, specialty additives, and other powdered substances that require meticulous handling. Key considerations in their design include preventing cross-contamination, managing dust explosion risks, and ensuring operator safety through enclosed filling mechanisms and robust sealing technologies.
Key Considerations in Chemical Powder Packaging
Selecting and operating powder packaging machinery in the chemical sector involves several crucial factors:
- Accuracy and Precision: Chemical formulations often require exact quantities. Machines must provide highly accurate weighing (gravimetric) or volume (volumetric) filling to prevent errors in composition and dosage.
- Dust Control and Containment: Many chemical powders are fine and can become airborne, posing health risks and environmental concerns. Effective dust collection systems and enclosed filling operations are paramount.
- Material Compatibility: The machinery must be constructed from materials resistant to corrosion, abrasion, and chemical reactions with the specific powders being handled. Stainless steel and specialized coatings are common.
- Safety Features: Automated systems should incorporate safety interlocks, emergency stops, and designs that minimize operator exposure to hazardous materials. Explosion-proof options may be necessary for certain environments.
- Sealing Integrity: The packaging must create a secure, airtight seal to prevent leakage, contamination, and maintain product stability during storage and transit.
- Regulatory Compliance: Equipment must meet or facilitate compliance with industry-specific safety, environmental, and product handling regulations.
Applications and Use Cases in the Chemical Sector
The versatility of modern powder packaging machines allows them to serve a wide array of applications within the chemical industry:
Specialty Chemicals
Packaging fine chemicals, catalysts, and additives where precision and purity are critical.
Agrochemicals
Filling pesticides, herbicides, and soil conditioners, often requiring dust-free operation.
Pigments and Dyes
Handling powders that can stain or be hazardous, necessitating contained systems.
Industrial Powders
Packaging materials like cement additives, metal powders, and construction chemicals.
Hygienic Powders
Solutions for food-grade chemicals, pharmaceutical ingredients, and other sensitive powders where hygiene is paramount.
Benefits of Automated Powder Packaging
Implementing automated powder packaging machines brings significant advantages to chemical manufacturers:
Enhanced Safety
Minimizes human exposure to potentially hazardous dusts and materials, reducing workplace accidents and health issues. Automated systems ensure consistent adherence to safety protocols.
Increased Efficiency
Automated processes operate at higher speeds and with greater consistency than manual methods, leading to higher throughput and quicker order fulfillment.
Reduced Operational Costs
Automating repetitive tasks lowers labor costs and minimizes material wastage due to inaccuracies, leading to a better return on investment.
Consistent Quality
Ensures uniform fill weights and high-quality seals on every package, maintaining brand reputation and customer satisfaction.
Buyer's Guide: Selecting the Right Powder Packaging Machine
Choosing the appropriate powder packaging machine requires careful evaluation of your specific needs:
Consider the nature of your chemical powder: Is it free-flowing, sticky, abrasive, or sensitive? This will determine whether an auger filler, vibratory filler, or another type of filling mechanism is most suitable. The particle size and density also play a role.
Determine the volume of product you need to package daily or hourly. This will influence the speed and type of automation required – from semi-automatic to fully integrated systems.
Evaluate the need for dust collection, explosion-proof features, and specific material construction (e.g., stainless steel) based on the hazardous nature of your chemicals and regulatory mandates.
What type of bags or containers will you use? Ensure the machine is compatible with your chosen packaging format and can achieve the required seal integrity for containment and shelf-life.
Think about how the packaging machine will integrate with your existing material handling systems. Do you need standalone machines, or a fully automated line with conveyors, bag placers, and checkweighers?
Quality and Reliability from Samirika Group
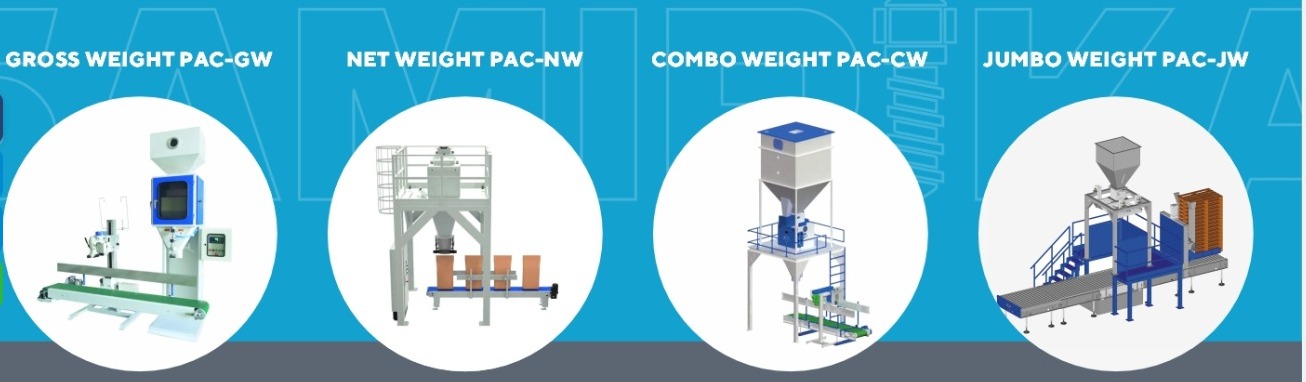
Samirika Group is dedicated to providing robust and efficient material handling systems, including advanced solutions for the chemical industry. Their range of automatic microprocessor-based controller-operated weighing and bagging systems are engineered to meet the rigorous demands of powder packaging. Whether you need precise weighing for sensitive chemical formulations or high-speed bagging for industrial powders, Samirika Group offers reliable equipment designed for accuracy, durability, and operational safety.
Their expertise extends to various packaging needs, including polymer packaging machines and jumbo packing machines, ensuring that manufacturers have access to a complete range of solutions. By focusing on automation and precision control, Samirika Group helps chemical businesses enhance their production efficiency, reduce costs, and maintain the highest standards of product quality and safety.
Frequently Asked Questions
What types of chemical powders can these machines handle?
These machines are designed to handle a wide spectrum of chemical powders, including free-flowing, semi-free-flowing, and some sticky or cohesive powders. Specific machine configurations can be tailored based on powder characteristics like particle size, density, and flowability.
How important is dust control in chemical powder packaging?
Dust control is critically important. Airborne chemical dust can be hazardous to human health, pose explosion risks, and lead to environmental contamination. Effective dust collection systems integrated into the packaging machine are essential for safety and compliance.
Can these machines handle hazardous or corrosive chemicals?
Yes, machines can be equipped with specialized materials, such as stainless steel or other corrosion-resistant alloys, and feature enclosed designs to safely handle hazardous or corrosive chemical powders. Specific configurations depend on the chemicals involved.
What level of automation is available?
Samirika Group offers a range of automation, from automatic microprocessor-based controller-operated weighing and bagging systems to fully integrated lines that can include automatic bag placers and bag pushers, providing solutions for various operational scales.
Ready to Enhance Your Chemical Powder Packaging Process?
Ensure the safety, accuracy, and efficiency of your chemical powder packaging operations. Explore the advanced material handling and packaging solutions offered by Samirika Group. Contact us today to discuss your specific requirements and find the perfect powder packaging machine for your chemical industry needs.
Learn More About Samirika Group Solutions